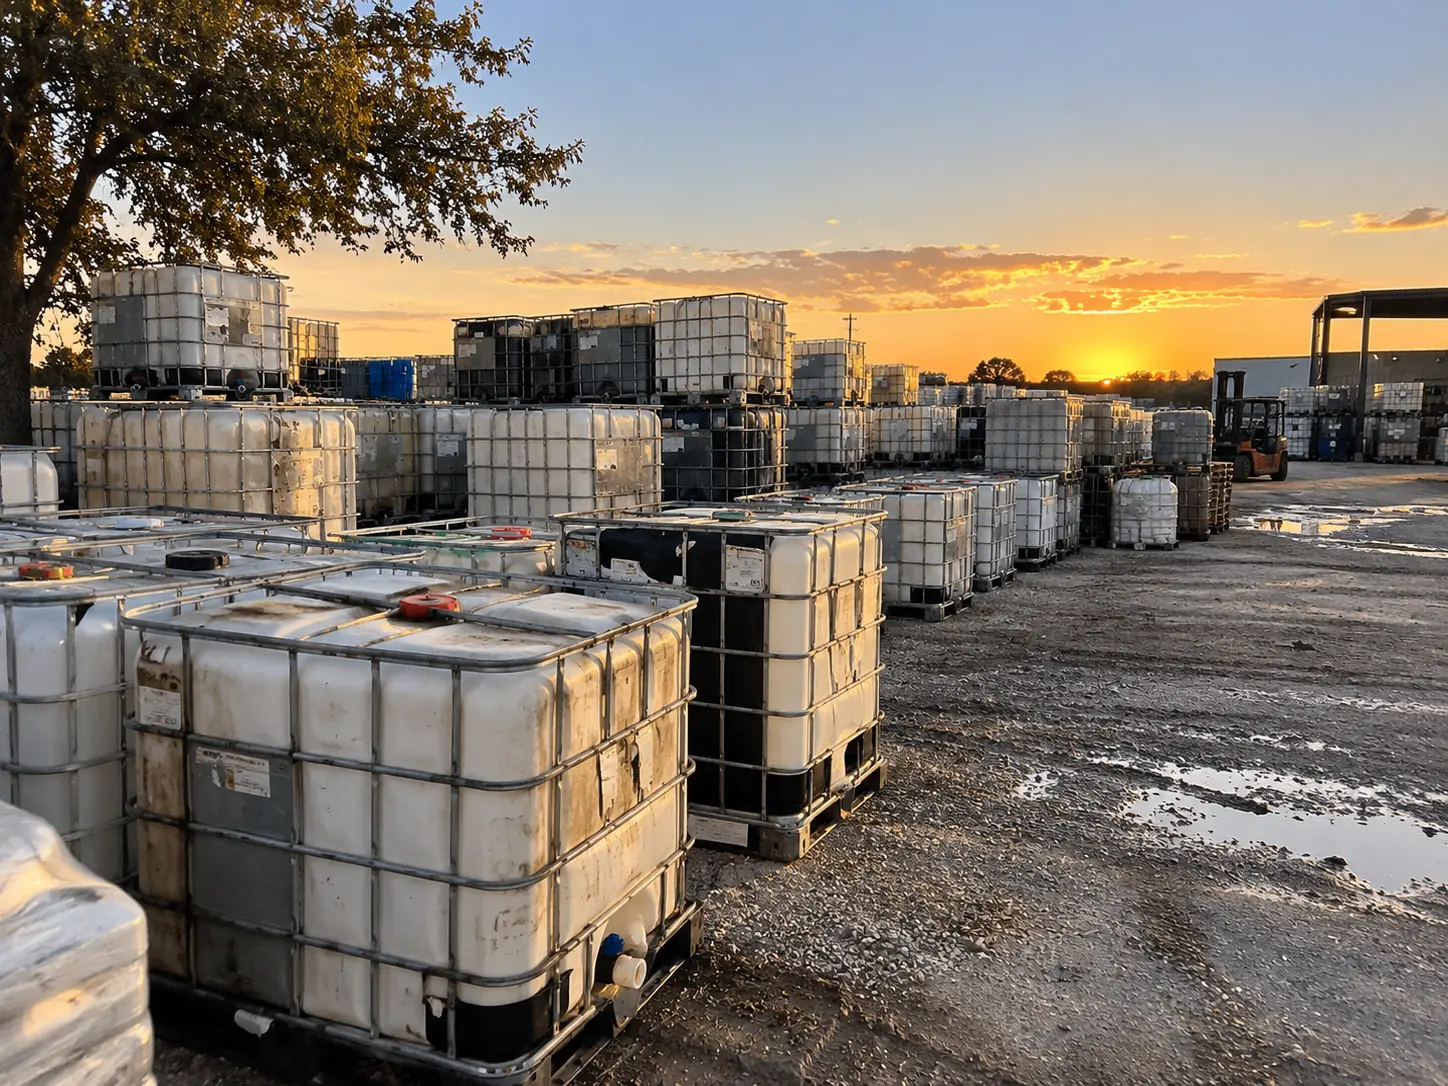
Polyethylene is not a barrier in the way glass or steel is a barrier. It is a semi-crystalline polymer: regions of tightly packed, ordered chains interspersed with amorphous regions where the chains are loose and disordered. Those amorphous regions have free volume between the chains, and small non-polar molecules can diffuse into that free volume and sit there.
That is permeation. It is not residue, it is not a film, and it is not on the surface. It is inside the wall of the bottle.
Why washing cannot reach it
A wash — any wash, at any temperature, with any chemistry — acts on surfaces. It dissolves, emulsifies or mechanically removes material sitting on the inside face of the bottle. Absorbed material is not sitting on that face; it is distributed through the first fraction of a millimetre of polymer and sometimes deeper.
Heat helps slightly, because raising temperature increases diffusion rates and some absorbed material will migrate out during a hot cycle. But a wash cycle is twenty-odd minutes and the migration timescale is weeks to months. You cannot bake a bottle clean in the time available without deforming it.
What permeates, ranked
Permeation into polyethylene correlates strongly with molecular size and polarity. Small, non-polar, lipophilic molecules go in readily. Large or highly polar molecules largely do not.
| Class | Examples | Permeation | Detectable afterwards |
|---|---|---|---|
| Terpenes | d-limonene, pinene, citrus oils | Severe | Yes — strongly, by odour |
| Chlorinated solvents | Perchloroethylene, methylene chloride | Severe | Yes — by odour, for years |
| Aromatic solvents | Toluene, xylene, mixed aromatics | High | Often, by odour |
| Fragrance and flavour concentrates | Essential oils, flavour bases | High | Yes, by odour |
| Aliphatic hydrocarbons | Mineral spirits, kerosene | Moderate | Sometimes |
| Dye and pigment carriers | Solvent dyes, tinting bases | Moderate | Yes, visibly as staining |
| Mineral oils | Lubricants, process oils | Limited | Occasionally, by feel |
| Glycols and glycol ethers | MEG, DEG, butyl cellosolve | Minimal | No |
| Surfactants | Non-ionics, anionics, detergent bases | Minimal | No |
| Aqueous inorganics | Brines, acids, caustics, fertilisers | Negligible | No |
The bottom three classes represent the large majority of industrial IBC traffic, which is why reconditioned totes work as well as they do in practice.
Staining is information, not a cosmetic defect
This is the most useful practical insight in this whole subject. A bottle with visible permanent staining is telling you that something permeated. That is bad news about that unit and good news about your ability to assess it — the risk is visible.
The genuinely dangerous unit is the one that looks pristine but held d-limonene for six months. There is no visual signal at all. Which is why the previous-contents declaration is the primary control and the visual inspection is the secondary one, not the other way round.
Treat staining as data. A stained tote has told you what happened to it. A clean-looking tote with no declared history has told you nothing, and nothing is worse than bad news.
How much actually migrates out
Honest answer: it depends on the substance, the contact duration, the wall thickness, the storage temperature and the time elapsed, and the published literature spans orders of magnitude. For most industrial applications the quantities are small enough to be irrelevant. For sensory-sensitive products they are not, because detection thresholds for some terpenes and aldehydes are in the parts-per-billion range.
- Weeks
- Absorption timescale in
- Months
- Migration timescale out
- ppb
- Sensory detection thresholds
- 0
- Washes that reverse it
That asymmetry is why the rule is binary rather than graduated. If your product has a sensory specification, you do not want a bottle with an unknown or incompatible fill history at any price.
Fluorination: a real but partial answer
Fluorinated HDPE has had its inner surface treated with fluorine gas, which replaces surface hydrogen atoms with fluorine and creates a barrier layer. It substantially reduces hydrocarbon permeation and it is a genuine engineering improvement, widely used for solvent and fuel service.
- It is a surface treatment, not a bulk property of the resin
- The layer is thin and not perfectly uniform across the bottle
- It degrades with repeated aggressive exposure rather than lasting indefinitely
- It reduces permeation substantially; it does not eliminate it
- For long contact times or many reuse cycles, stainless remains the durable answer
Buying around the problem
There are four strategies, in ascending order of cost and certainty. Most buyers need the second one and ask for the fourth.
- 01Restricted allocation. Ask your supplier to allocate only units whose entire declared fill history is compatible with your product. This costs nothing but lead time and solves most cases.
- 02Rebottled stock. A new bottle in a reclaimed cage. The contact surface has never held anything, so permeation does not arise, at roughly 44% of the embodied carbon of a new unit.
- 03New stock. If a specification requires a certificate of virgin assembly, this is the route — but understand you are buying a certificate, because a rebottled bottle is equally unused.
- 04Stainless steel. Zero permeation, steam-cleanable, a hundred-plus service lives. Only economic in a controlled return programme where you actually get the unit back.
What to ask for, concretely
If permeation is a live concern for your product, these are the four things worth having in writing from a supplier.
- The declared previous contents, per unit, not per lot
- The wash programme code that ran on each unit
- Confirmation of whether any unit in the lot held a terpene, aromatic or chlorinated solvent, or a fragrance or flavour concentrate
- Agreement that units failing that screen will be substituted rather than supplied with a caveat
A supplier who can produce all four is managing permeation deliberately. One who cannot produce any of them is managing it by hoping, and you will find out which eventually — three weeks after a fill, when the arithmetic is hardest to do.